
Technical conferences and factory visits are easy to report as ceremonial events. Their real value is more demanding: can a research question be translated into a measurable production control, and can shop-floor evidence help researchers focus on problems that matter in practice? A recent source article described an academic and technical exchange in Inner Mongolia followed by a visit to a steel fabrication facility. Participants discussed topics such as non-destructive testing, structural monitoring, defect detection and quality control.
For overseas owners, EPC contractors, engineers and steel buyers, the transferable insight is not the attendance list. It is the potential of a steel fabrication quality feedback loop connecting design assumptions, production conditions, inspection data, corrective actions and future process improvement. This article develops that practical lesson while avoiding unsupported claims about capacity, certifications or overseas delivery capability.
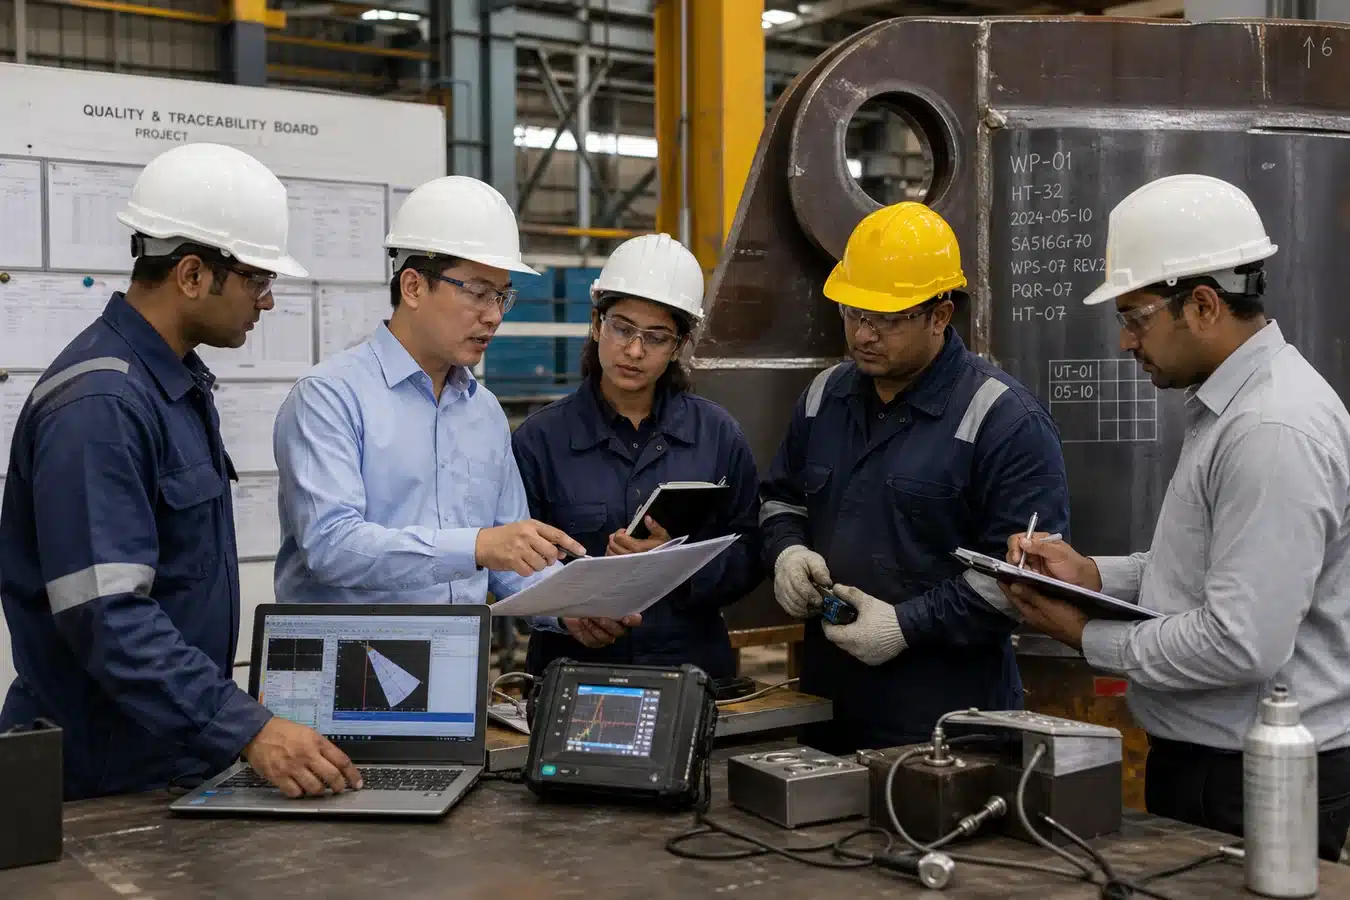
Begin with a defined production question
Collaboration is most useful when it begins with a problem that can be observed and measured. “Improve welding quality” is too broad. Better questions include: Which joint configurations generate repeated repairs? Does a particular inspection indication correlate with fit-up or heat-input variation? Where does dimensional drift enter an assembly? Which coating defects occur after handling rather than application?
A focused question determines what data to collect and who needs to participate. Engineers understand design intent; operators understand practical constraints; inspectors see recurring indications; researchers can help structure analysis. Without a defined question, a factory tour produces impressions but little evidence.
Map controls across the fabrication route
A process map helps teams locate where quality is created and where information is lost. A typical structural steel route may include material receipt, identification, cutting, forming, fit-up, welding, correction, surface preparation, coating, dimensional inspection, packing and dispatch. Actual routes vary by product and facility.
At each stage, the team can identify inputs, process variables, acceptance criteria, records and handover conditions. This exposes gaps such as material marks lost after cutting, an inspection result not linked to a member, or a coating repair recorded without location. It also prevents disproportionate attention to final inspection when the root cause lies earlier.
Use NDT as part of an engineering decision system
Non-destructive testing is often discussed as a collection of methods. In practice, method selection should follow the material, joint geometry, likely discontinuity, access and governing acceptance criteria. Visual testing is foundational. Other methods may include ultrasonic, radiographic, magnetic-particle or penetrant testing where suitable and specified.
More testing is not automatically better. An examination must be technically appropriate, performed by qualified personnel and interpreted against the correct standard. The inspection plan should define extent, timing, location identification, reporting and response to nonconformity. If research introduces a new sensing or analysis method, it should be validated for the intended task before it influences acceptance decisions.
Connect inspection data to process conditions
An isolated NDT report says whether an examined area met stated criteria. A connected dataset can support prevention. Weld location, joint type, material, thickness, procedure, operator, fit-up condition, shift, consumable batch, inspection method and result may all be relevant. Data collection should remain proportionate and respect commercial and personnel confidentiality.
The aim is not to rank individuals from a small sample. It is to find repeatable patterns. If similar indications cluster around one detail, the detail or access may deserve review. If distortion recurs after a particular sequence, production engineering can test an alternative. If no reliable relationship exists, the team should avoid forcing a conclusion.
Create a closed corrective-action loop
| Step | Key question | Output |
|---|---|---|
| Detect | What condition was observed, where and by which method? | Traceable nonconformance record |
| Contain | Which components or processes could also be affected? | Defined hold and review scope |
| Analyze | What evidence supports the likely root cause? | Cause analysis |
| Correct | How will the specific item be restored under approval? | Repair or disposition record |
| Prevent | What process, detail, training or control should change? | Approved action plan |
| Verify | Did recurrence and risk actually decrease? | Effectiveness review |
Closing the loop is essential. A repair that passes reinspection resolves one component but may leave the process unchanged. Conversely, a broad procedure change based on one unusual event may add cost without benefit. Decisions should match the evidence and risk.
Make factory visits evidence-based
A client, academic or technical visit should be planned around selected processes and records rather than a polished route alone. Visitors can follow one member mark from material receipt through current production, examine how revision status is controlled, observe inspection access and ask how nonconformities are handled.
- Select representative components before the visit.
- Agree confidentiality and photography rules.
- Review the applicable process and inspection documents.
- Observe actual work without interrupting safe operations.
- Compare records with markings on the physical component.
- End with actions, owners and realistic completion dates.
This approach is equally useful for a buyer audit and a research exchange. It grounds discussion in observable work while avoiding unsupported generalizations from a staged demonstration.
Evaluate digital tools by the decision they improve
Digital twins, automated inspection, sensing and analytics can be valuable, but each tool needs a defined use case. What decision will it support? What data quality is required? How will results be validated? Who owns the data, and how will configuration changes be controlled?
A simple traceable weld map may solve a current problem better than a complex platform with inconsistent inputs. Technology should reduce uncertainty or response time, not merely increase the amount of data collected. Pilot projects need baseline performance and pre-agreed success measures.
Translate learning into procurement assurance
Buyers benefit when continuous improvement is visible in project controls. Tender reviews can ask how a supplier analyses recurring nonconformities, updates procedures and verifies effectiveness. During production, dashboards should focus on meaningful indicators such as closure time, recurrence, traceability completeness and release status—not a single headline pass rate detached from inspection scope.
None of these practices proves that a company possesses a particular certification, scale or international installation capability. Those claims require separate, current evidence. Research collaboration and technical dialogue are valuable because they can strengthen how problems are framed and solved, not because attendance itself certifies delivery performance.
A practical agenda for the next technical exchange
Choose one production problem, define the evidence needed, observe the process, review anonymized data, agree a limited intervention and measure its effect. Document what worked, what did not and what remains uncertain. This cycle creates knowledge that engineers and workshop teams can both use.
Quality improves when information travels in both directions: research into production, and production evidence back into analysis. To discuss quality documentation and inspection expectations for a structural steel package, please Contact Us.